Explore our high-purity, standardized plant extracts customized for commercial formulation and regional wholesale distribution in Grenville.
Navigating clean-label demands, raw material stability, and enterprise supply chains across Grenville and surrounding trade routes.
Grenville’s expanding commercial sector—spanning artisanal food processing, functional beverage blending, sports nutrition manufacturing, and cosmetic formulating—requires scalable, pathogen-free, highly soluble fruit ingredients. Raspberry powder (Rubus idaeus) has become a centerpiece ingredient due to its natural anthocyanin content, vibrant natural color, subtle acidity, and clean-label appeal. Our supply network ensures uninterrupted delivery schedules, standardized mesh sizes, and low-moisture stability optimized for Grenville's local manufacturing climate.
Procuring raw botanical ingredients in Grenville often presents logistical bottlenecks, such as batch-to-batch color variation, caking caused by high humidity, residual pesticide compliance issues, and fluctuating bulk costs. UniCare resolves these friction points by delivering micro-milled, spray-dried, and freeze-dried raspberry powders produced under automated quality management systems. Every batch delivered to Grenville comes backed by exhaustive COAs covering heavy metals, micro-biology, and solvent residues.
Global Excellence in Natural Active Ingredients & Herbal Processing
UniCare is a professional supplier of natural active ingredients. Our products are widely used in various fields such as dietary supplement, food, cosmetics, and pharmaceuticals. We focus on product development and quality stability, and insist on growing together with our customers around the world, including manufacturing enterprise partners in Grenville.
UniCare has deep cooperation with several excellent Chinese manufacturers who have complete quality management system certifications, including but not limited to GMP, EUGMP, CEP, ISO9001, ISO22000, and HACCP. Each factory has independent testing capabilities and is equipped with advanced and efficient testing equipment to ensure the high quality and long-term stability of each batch of products.
Driving technological breakthrough and corporate responsibility in botanical science
Discover and create the new value of herb for modern health and wellness applications globally.
Continuous innovation and improvement across extraction, isolation, and powder milling systems.
Utilize the most advanced technology to produce the highest quality products for international clients.
Make the employees happy and give back to the community through sustainable sourcing practices.
Why Leading Grenville Enterprise Buyers Trust UniCare's China Production Base
UniCare attaches great importance to the hardware conditions of production equipment and has the largest and most advanced extraction factory in China. The entire production line in UniCare is controlled by a modern, intelligent, dynamic automatic control system. Until now, UniCare has built up two GMP workshops, containing six multi-functional extraction lines, among which there is the only production line for Ginkgo Biloba Extract of acetone process in the whole China. Here are several other production lines including fermentation production lines and Chinese medicine pieces. A total of 30,000 tons of various Chinese medicine plant raw materials can be processed each year.
The facility has fully passed China GMP certification, adhering strictly to cleanroom environmental and operational standards.
The EU-GMP and CEP certifications of key botanical extracts highlight our benchmark quality execution.
All extraction production lines feature modern, intelligent, and automated control systems to prevent human error.
State-of-the-art countercurrent extraction units allow maximal retention of fragile active compounds like anthocyanins in raspberry powder.
Annual processing capacity of 30,000 tons guarantees price stability and year-round volume availability for Grenville procurement.
Six 20-ton capacity fermentation tanks for enzyme-modified products and specialized bio-transformed botanical nutrients.
Providing custom mesh, solubility, and functional parameters for diverse downstream sectors.
Grenville beverage manufacturers utilize our 100% water-soluble spray-dried raspberry powder to impart natural ruby hue, distinct flavor profiles, and antioxidant power into RTD teas, kombucha blends, functional waters, and craft cocktails without creating sediment.
Formulators in Grenville incorporate our freeze-dried raspberry powder into berry antioxidant blends, meal replacements, and immune-support sachets. Rich in Vitamin C, ellagic acid, and polyphenols, it strengthens product claim integrity.
With high natural skin-soothing properties and vitamin content, top-tier skincare brands serving Grenville order fine-mesh organic raspberry powder for anti-aging masks, face scrubs, and natural pigmentation formulations.
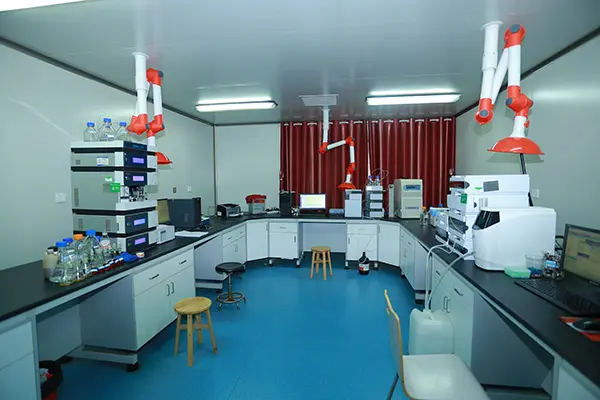
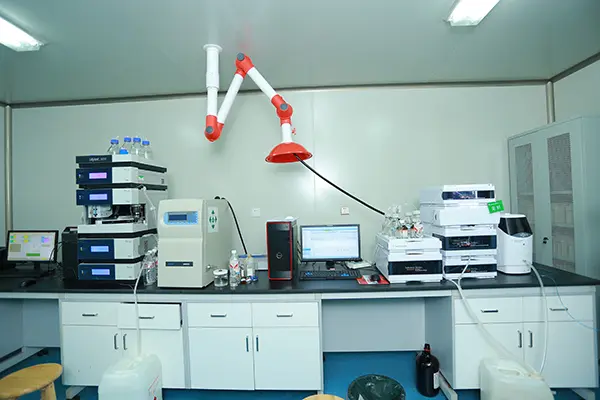
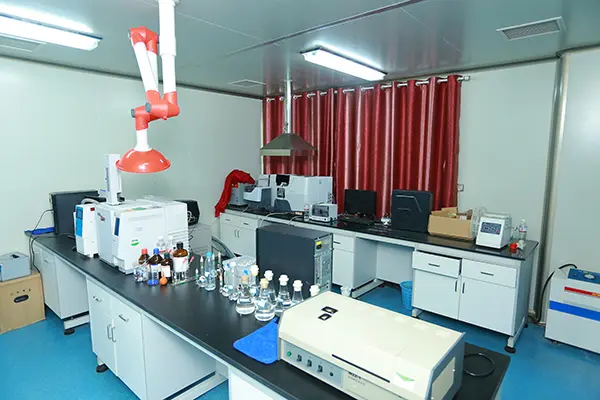
CNAS Qualified Central Laboratory Ensuring Uncompromised Purity and Safety
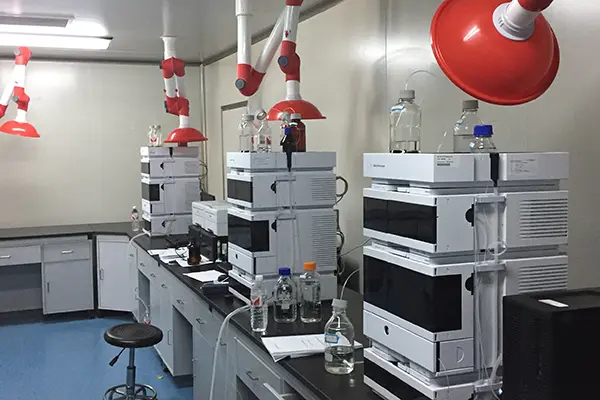
UniCare has established a leading and complete quality control system, strictly maintaining high product standards. With advanced testing instruments, we perform exhaustive checks to provide every Grenville customer with premium, fully verifiable products.
Detectable Parameters Include: Active/Signature component detection (HPLC or UV), solvent residues (GC), pesticide residues (organochlorine GC-MS-MS), heavy metals (Lead, Arsenic, Mercury, Cadmium, Copper via ICP-MS), microscopic identification, moisture, dry weight loss, ash content, microbial limits, thin layer identification (TLC), bulk density, conductivity, pH value, and sulfur dioxide residue.
| Testing Category | Analytical Scope & Target Parameters |
|---|---|
| Active Ingredient Analysis | Assay content, purity identification via standardized HPLC/UV profiles. |
| Hazardous Substance Analysis | Heavy metals (ICP-MS), pesticide residues screening (400+ compounds), residual solvents. |
| Microbe Analysis | Total plate count, Escherichia coli, Salmonella, Yeast & Mould, specific pathogen limits. |
| Raw Material Control | GACP origin traceability, allergen screening, non-GMO status, botanical authenticity verification. |
| Regulatory Compliance | Verification according to EU, USP, EP, and local target market food & drug regulations. |
| Stability Testing | Accelerated and real-time shelf-life testing under temperature/humidity stress. |
| Physical Properties | Particle size distribution (mesh degree), bulk density, solubility rate, moisture, ash content. |
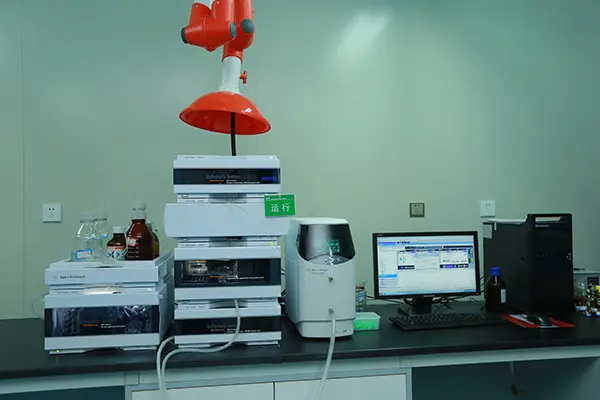
Our CNAS-qualified laboratory operates top-tier analytical machinery to ensure every batch of Raspberry Powder and herbal extract sent to Grenville matches international pharmacopeia standards:
| Instrument Name | Quantity | Application Focus |
|---|---|---|
| UHPLC, Agilent 1290 | 2 Units | Ultra-High Performance Liquid Chromatography for ultra-fast active ingredient identification. |
| HPLC, Agilent 1260 | 4 Units | High Performance Liquid Chromatography for assay standardization and marker quantification. |
| HPLC, Shimadzu LC-20AT | 2 Units | Purity testing, bio-active constituent profile mapping, TLC validation. |
| ELSD, Shimadzu 2000ES | 2 Units | Evaporative Light Scattering Detection for non-chromophoric compound analysis. |
| Gas Chromatograph, Shimadzu GC-2010 | 1 Unit | Organic solvent residue determination and volatile oil profiles. |
| Atomic Absorption System, Shimadzu AA-7000 | 1 Unit | Trace element heavy metal quantification (Pb, Cd, As, Hg). |
Ensuring Sustainable Sourcing, High Yield, and Product Innovation
UniCare invests 10% of our annual net profit into research and development. In addition to optimizing existing natural plant extraction processes, we have established a dedicated R&D department for natural fermentation products. By increasing investment in fermentation technology, we break through traditional extraction limits to drive industry evolution.
Furthermore, UniCare works in deep technical cooperation with Beijing University of Chemical Technology in fermentation science, jointly developing and converting novel pharmaceutical, cosmetic, and nutraceutical raw materials into full-scale industrial production.
To control raw material quality at the origin, UniCare maintains a stringent procurement system extending directly to agricultural soil plots, allowing total batch traceability. Raw material storage follows advanced quality management processes, strictly checking active constituents, moisture, ash, heavy metals, and pesticide residues.
We co-manage dedicated planting bases (including Ginkgo leaf, Epimedium, Phellodendron, and Olive leaf bases) following GACP (Good Agricultural and Collection Practice) guidelines. Collaborating with seedling research institutions, we optimize plant genetics to boost active yields and lower unit cost for our B2B partners in Grenville.
Streamlined logistics, custom OEM/ODM packaging, and dedicated regulatory support.
We supply pure 100% Freeze-Dried Raspberry Powder or custom Spray-Dried Raspberry Powder with organic maltodextrin/tapioca carriers adjusted to your exact solubility, density, and flowability requirements in Grenville.
From 1kg vacuum foil bags for clinical trial batches to 25kg fiber drums with double food-grade polyethylene liners, we offer tailored packaging options suited for long-distance ocean and air transport to Grenville.
Our international logistics team coordinates seamless door-to-door or port-to-port shipments to Grenville, providing complete shipping documentation including Bill of Lading, COA, Phytosanitary Certificate, and Certificate of Origin.
Everything you need to know about ordering bulk Raspberry Powder and botanical extracts for Grenville.
Browse our expanded range of standard and specialized botanical extract products available for wholesale supply.
Contact our technical sales team today to request Certificate of Analysis (COA), specification sheets, or custom batch formulations of Raspberry Powder and herbal extracts tailored for your Grenville facilities.
Send Inquiry Now